


 Back

Recently, the project undertaken and implemented by Hefei EPANEL Water Supply Technology Co., Ltd.Xinjiang Beishan Mining Co., Ltd. underground fire protection and production water tank pumping station projectAll installation and commissioning work was successfully completed, and the entire BDF prefabricated box-pump integrated fire water supply system reached the design and operation standards, building a stable and reliable fire water supply guarantee system for safe production in the mining area.
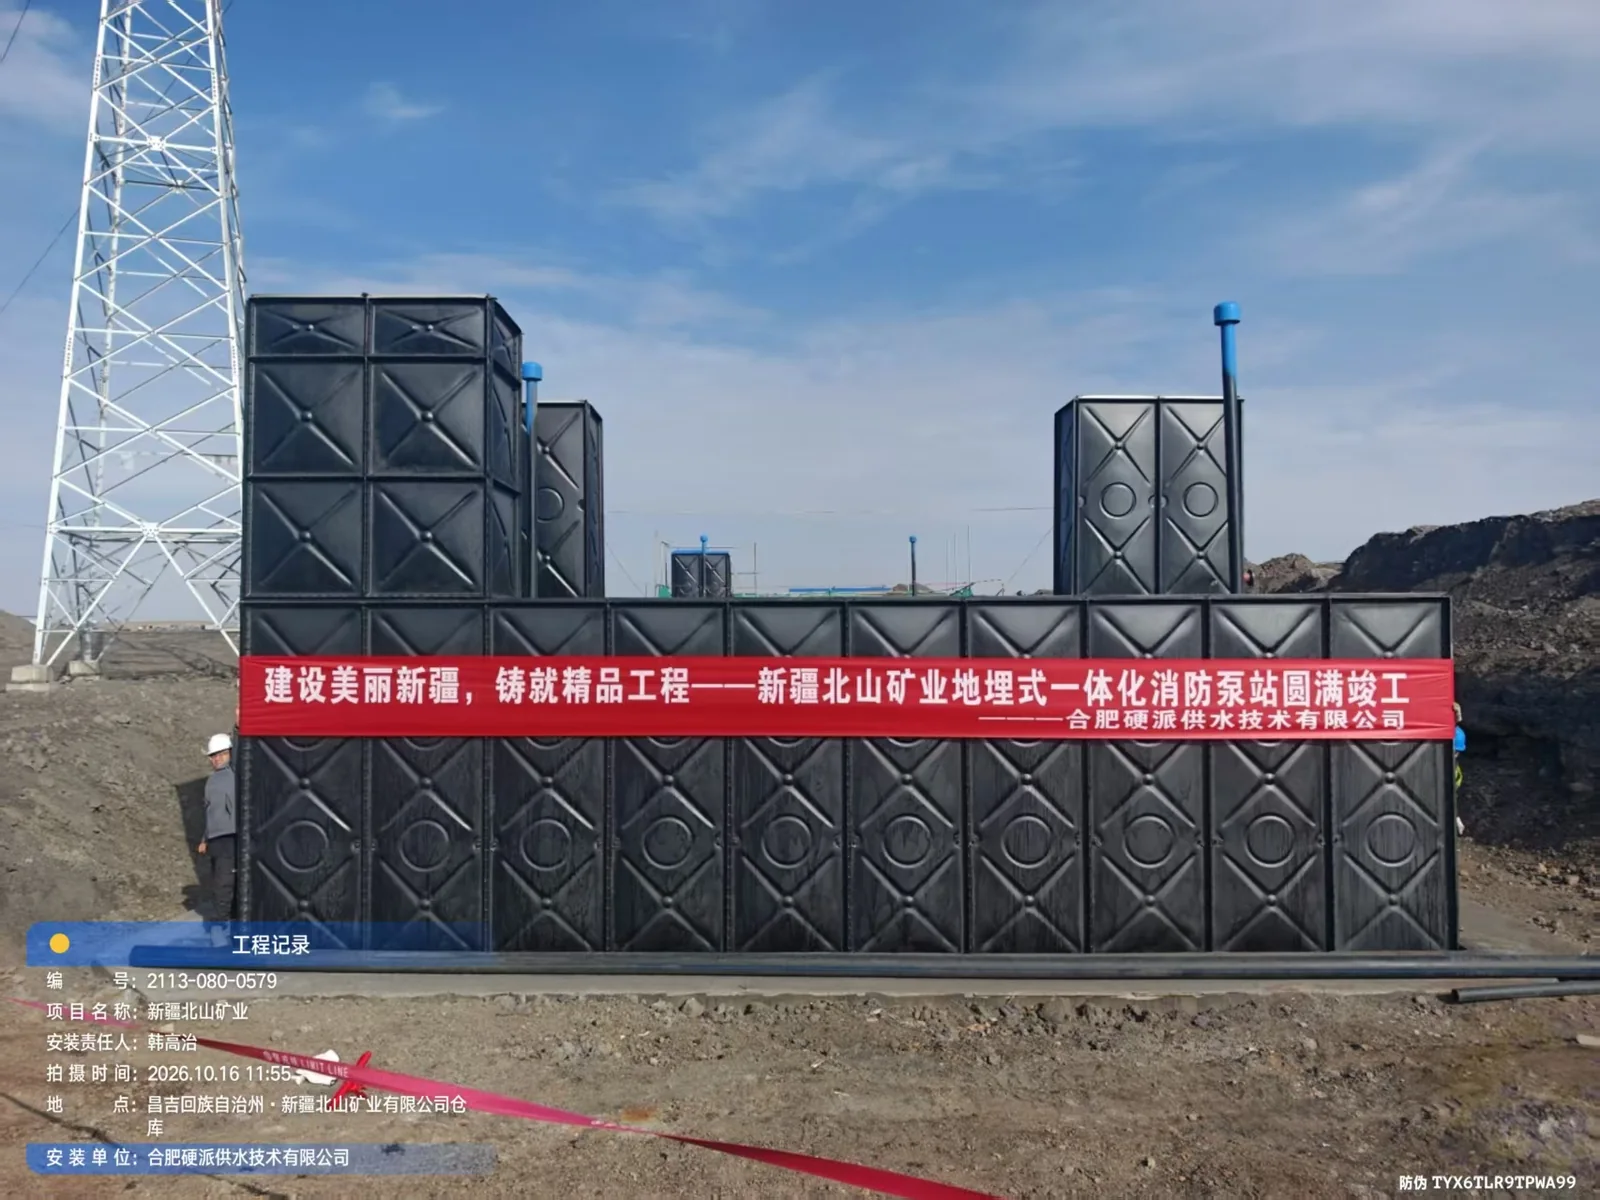
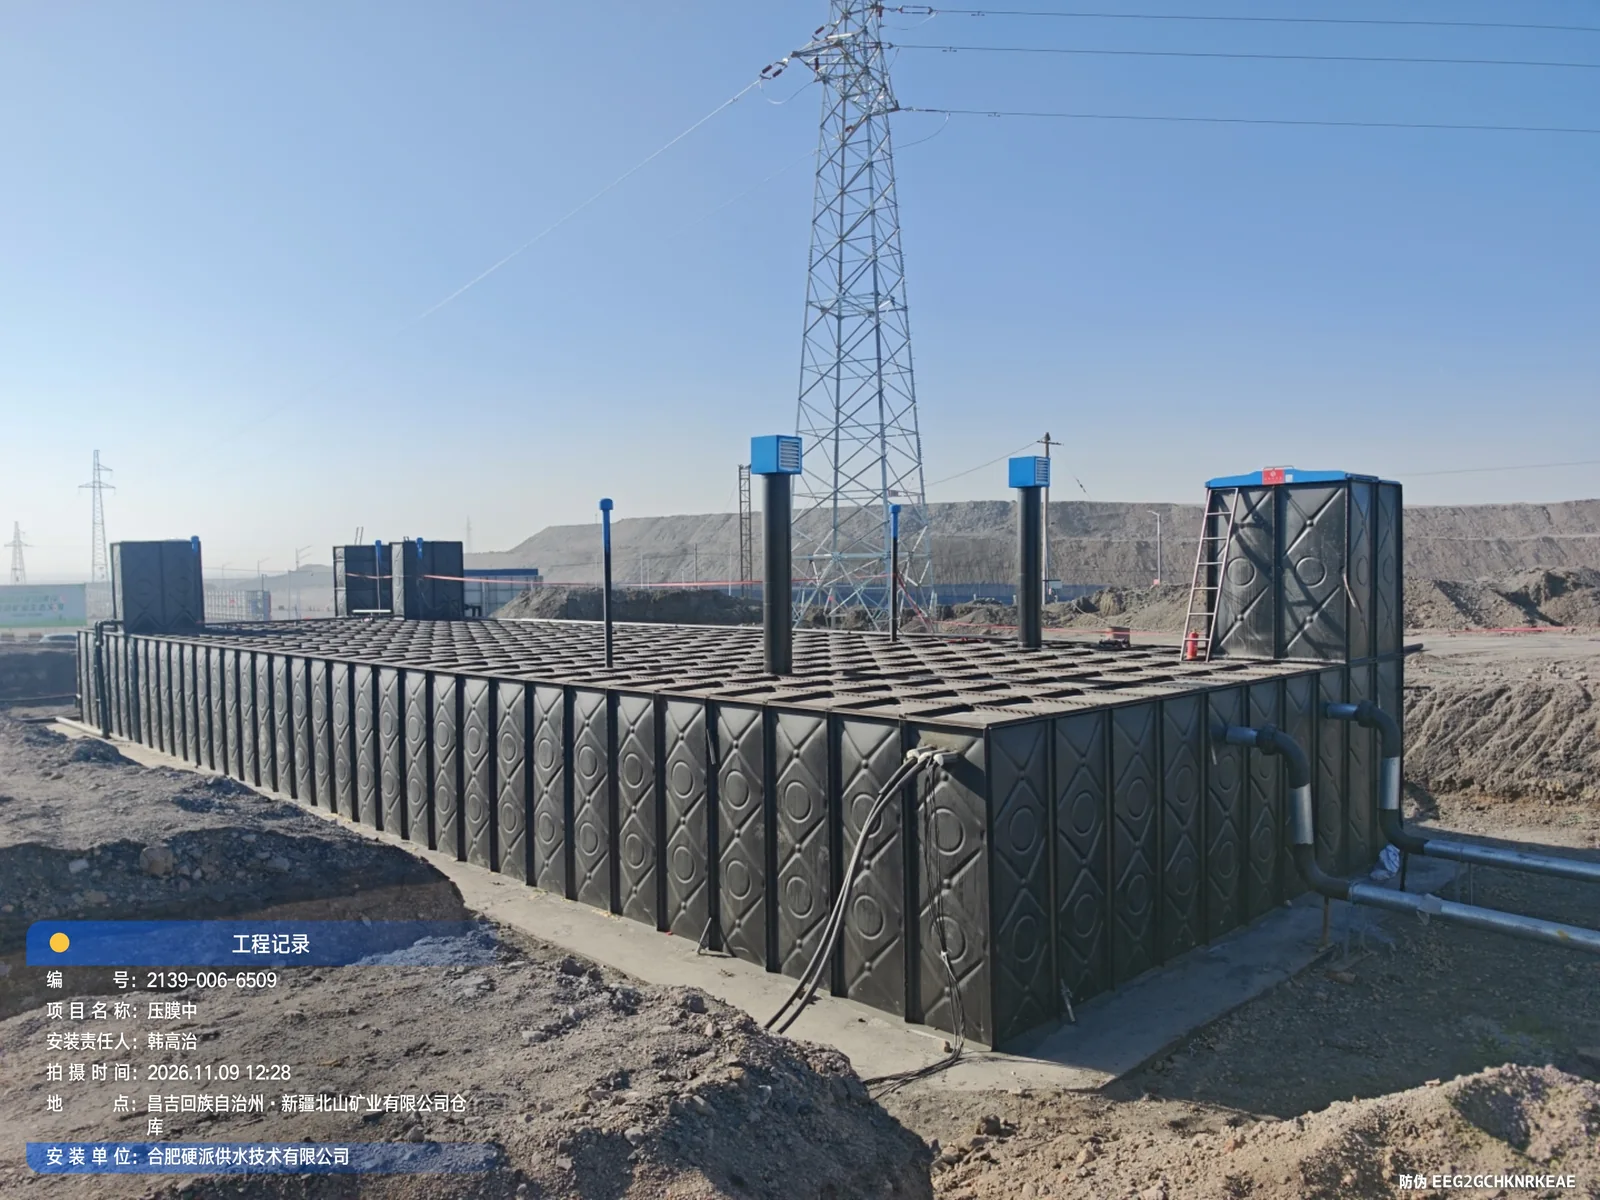
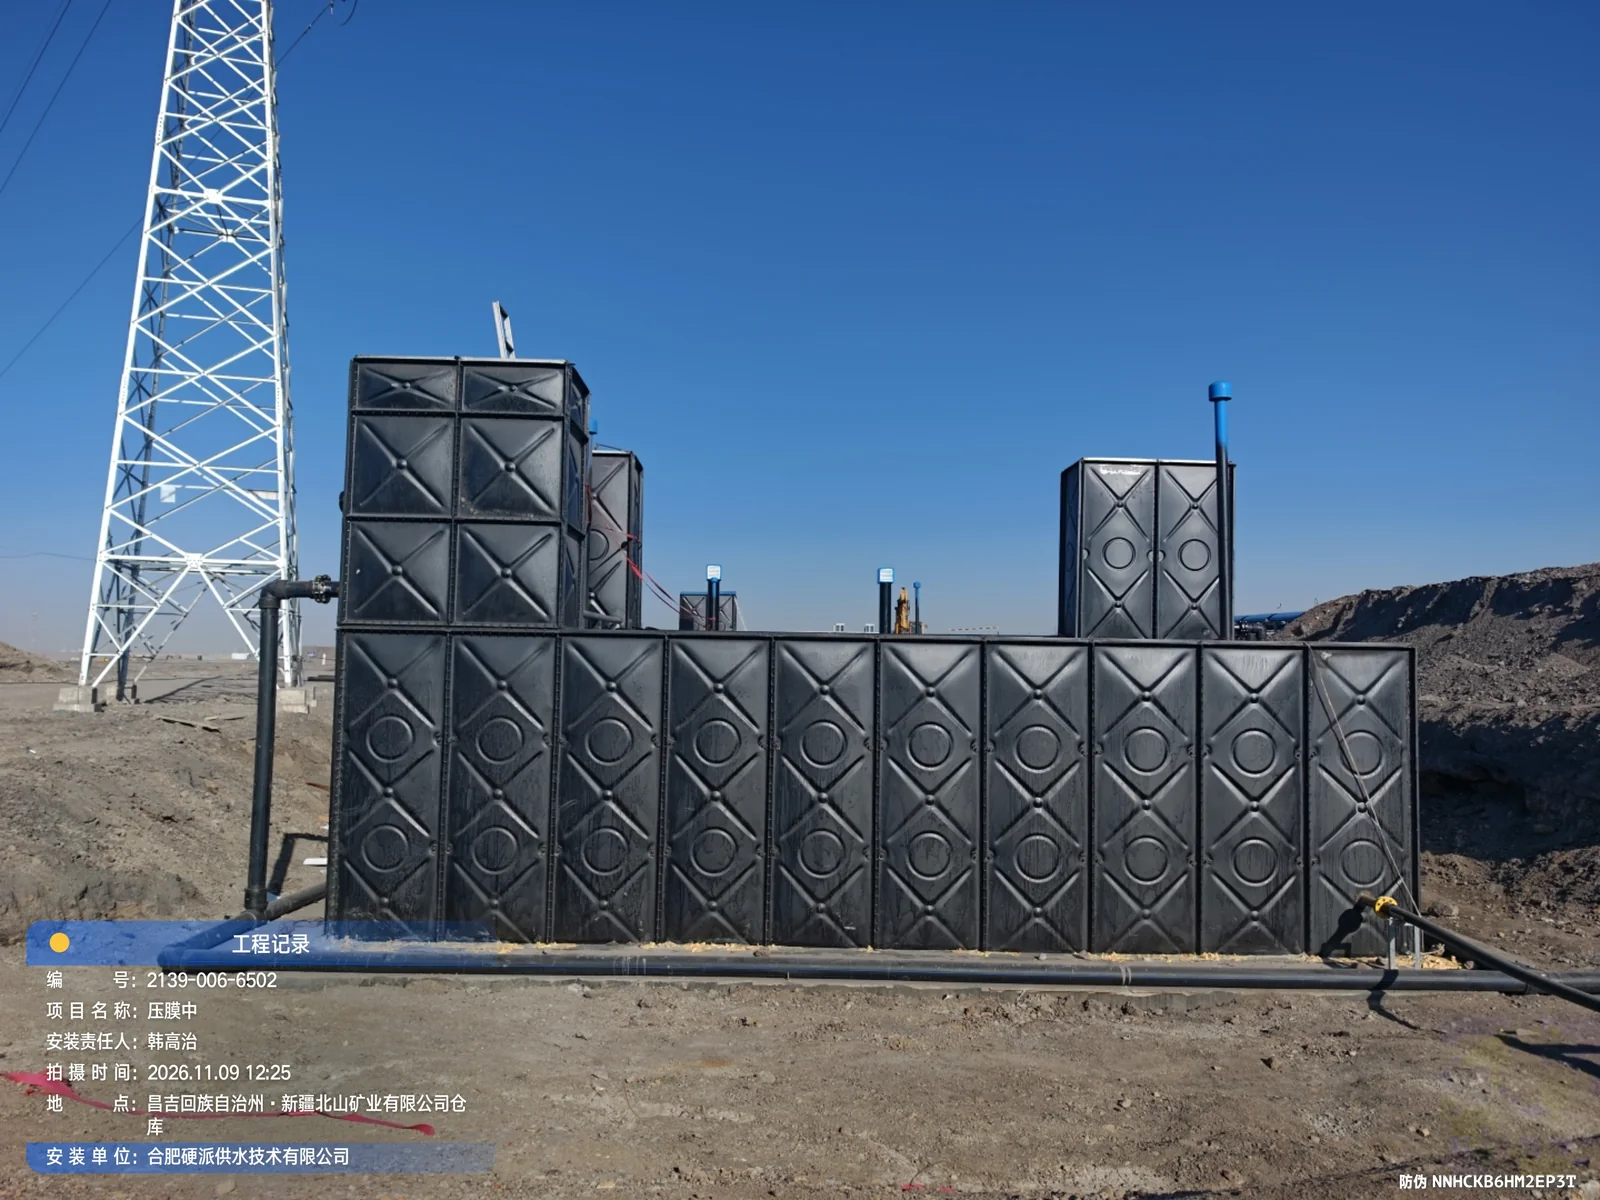
This project adopts the MX intelligent prefabricated tank pump integrated solution. The overall dimensions of the pump station are 31m×10m×3m. It is composed of a fire water tank and an integrated pump room. The pump room area specifications are 6.0m×10.0m×3.0m. The nominal volume of the water tank is 750m³, the effective volume is 637.5m³, the box specifications are 25m×10m×3m+6m×10m×3m, and it adopts a double-column structure design; the water tank side panels are made of 4.4mm BDF composite board, pump room side panels 4.0mm galvanized sheet, equipped with a complete set of accessories such as water tank ladders, maintenance manholes, water inlet and outlet openings, unpowered ventilators, equipment room sliding doors, steps, etc. The project scope covers materials, production, transportation, on-site installation, etc., and the internal pipelines and valve systems of the pump room are constructed simultaneously.
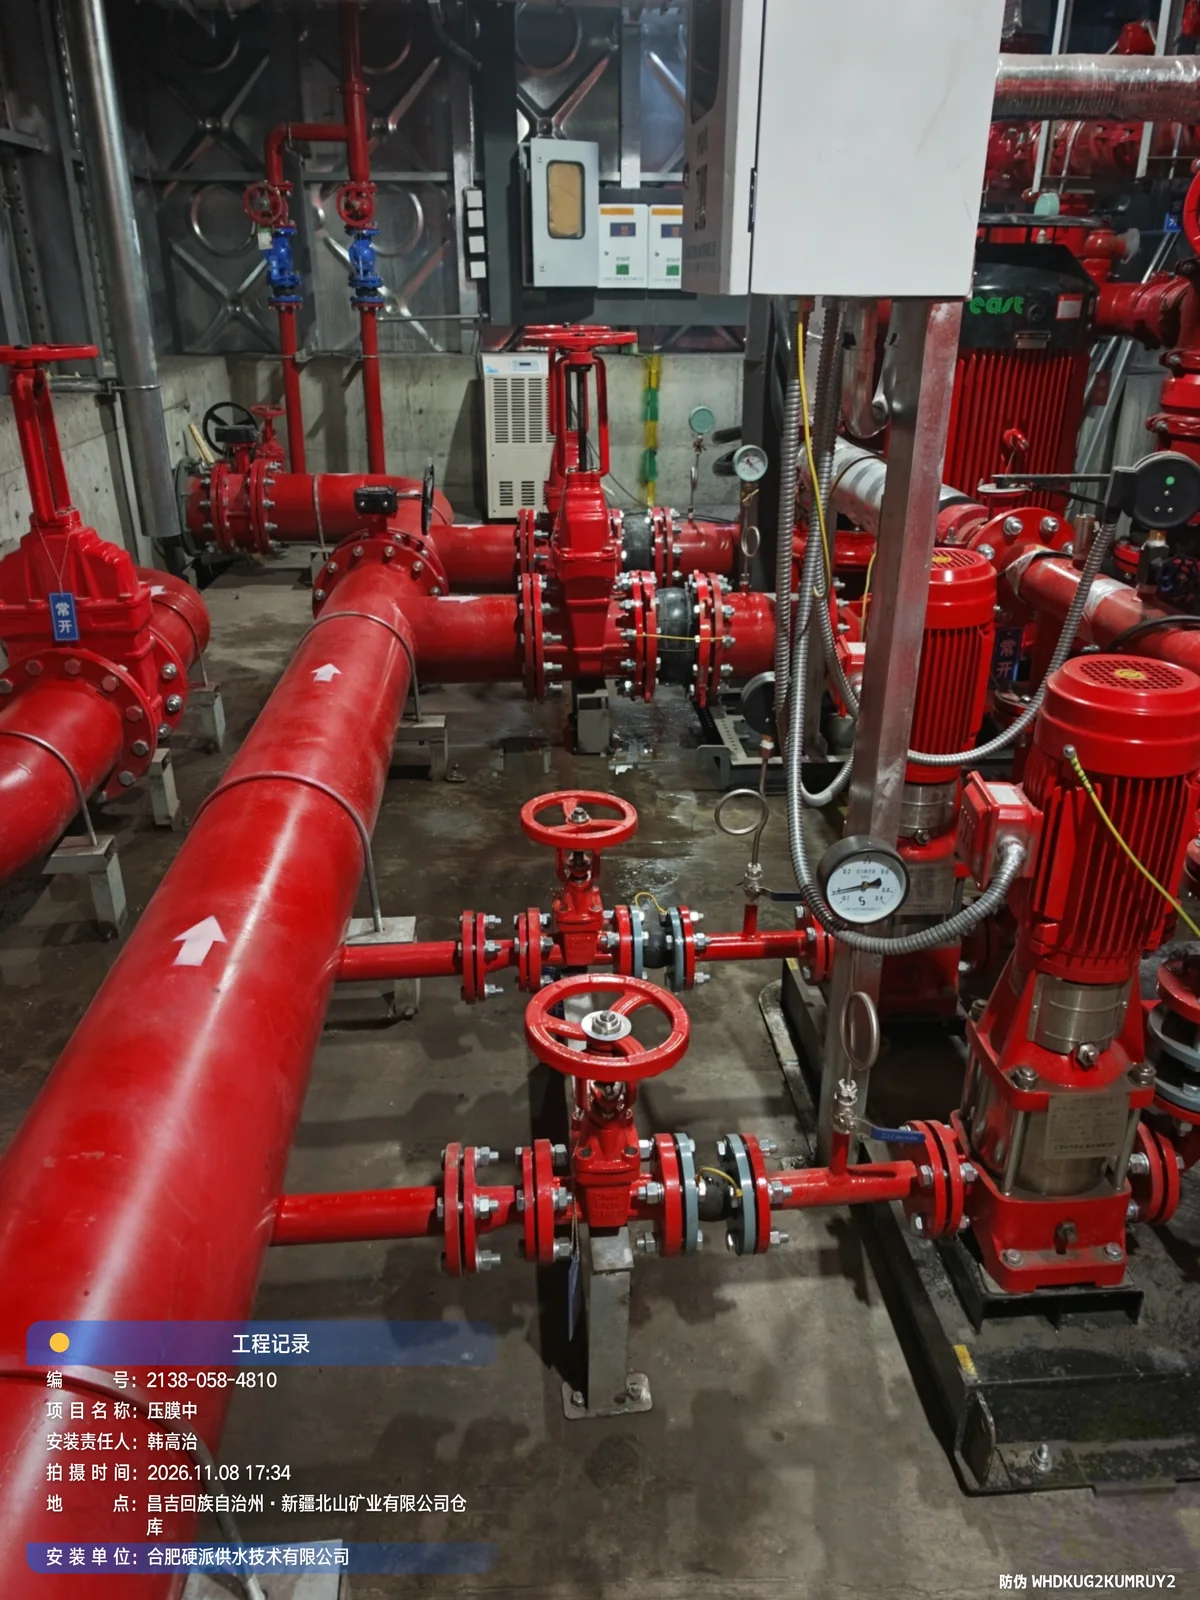
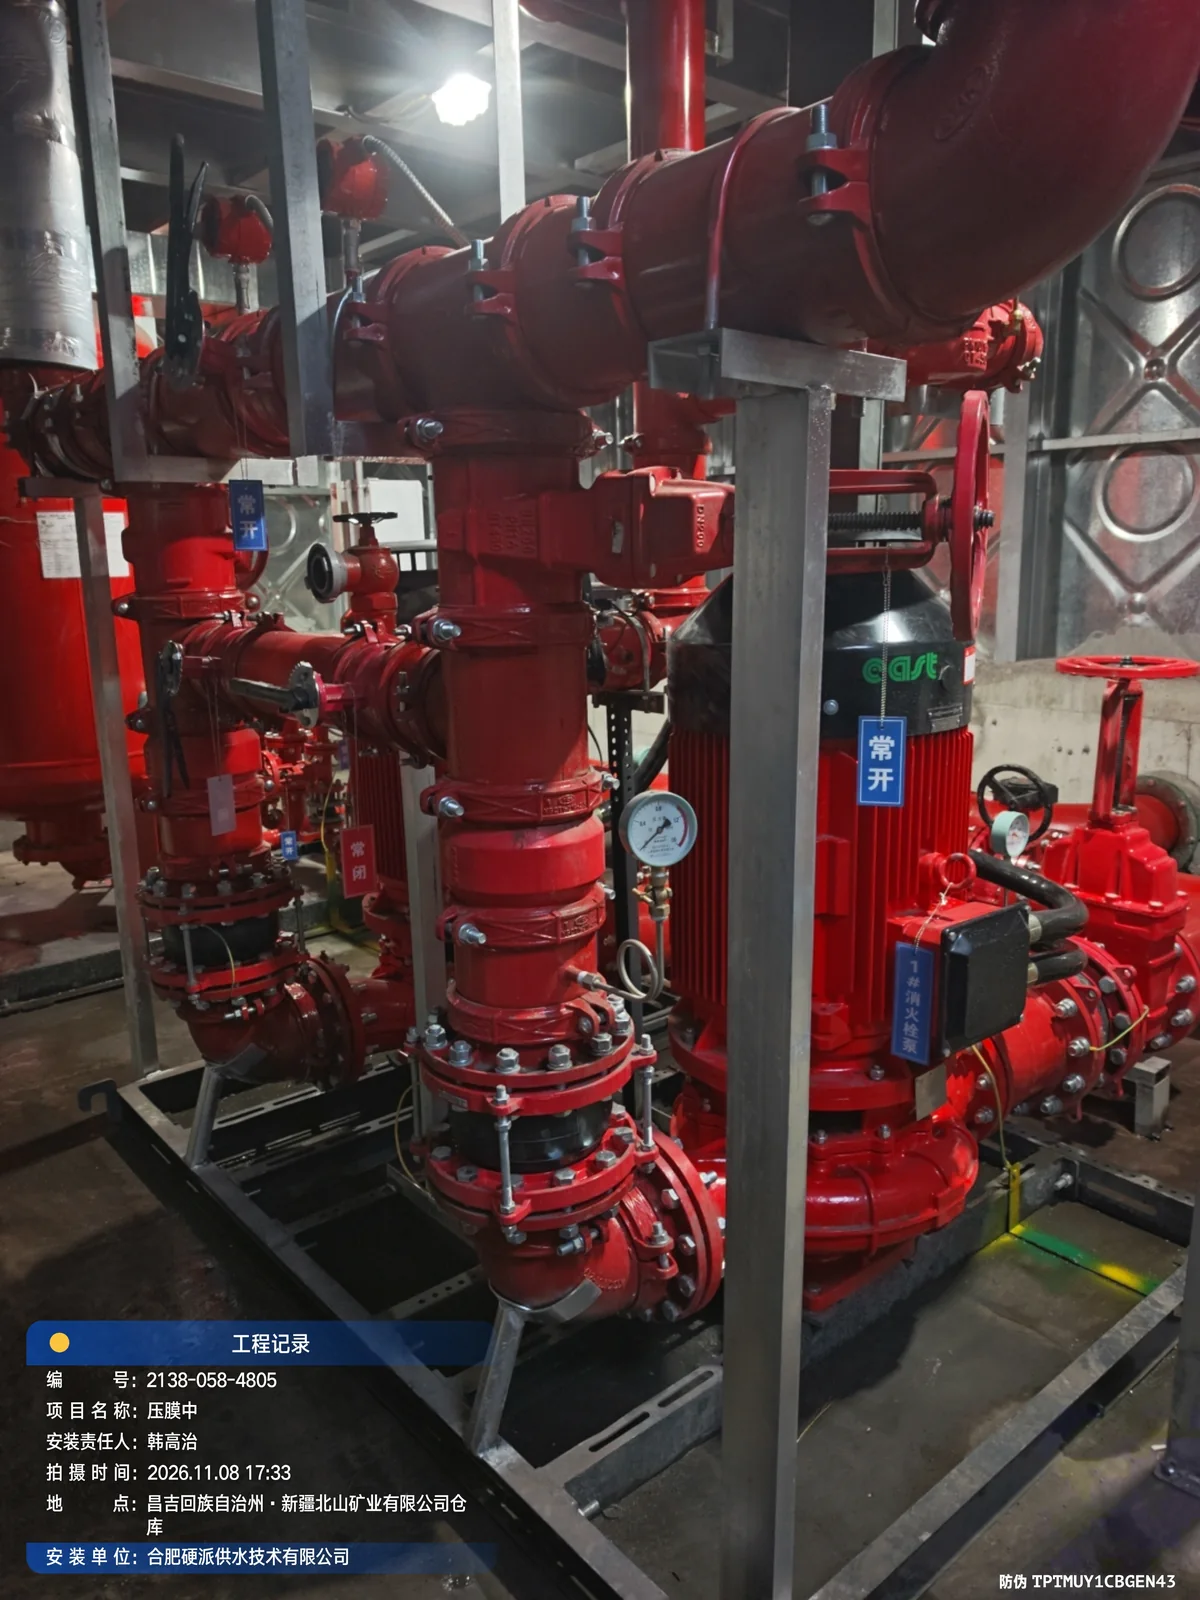
The station uses 2 XBD4.0/60G-200-75-G electric main fire pumps rated at 60 L/s, 40 m head and 75 kW, with a pump separation of at least 1200 mm. The W7.2/45-2.2 jockey pump assembly includes an XBD4.5/2W-DFCL-2 jockey pump rated at 2 L/s, 45 m head and 2.2 kW, an SQLC1000-0.6 hydropneumatic tank, and a DFK2.2-2BP-CT-A control cabinet. The installation also includes 2 80WQ11142 sewage pumps rated at 36 m³/h, 15 m head and 3 kW, with a dedicated control panel. The fire control system includes a DFK-XFYJ75-2J-F fire electrical controller, a CCCF-certified DFK-XH-250/K4 dual-supply cabinet and a DFK-X-6V4 inspection cabinet. The dual-supply cabinet has 7 branch switches, a GST-DJ-S63C power monitor, instrument transformers, fuses, and associated accessories. The inspection cabinet protects the pump room against flooding and provides tank inlet control for 3 interlocked DN300 motorized valves. EPANEL supplies the valves, whose main and control circuits connect to the inspection cabinet.
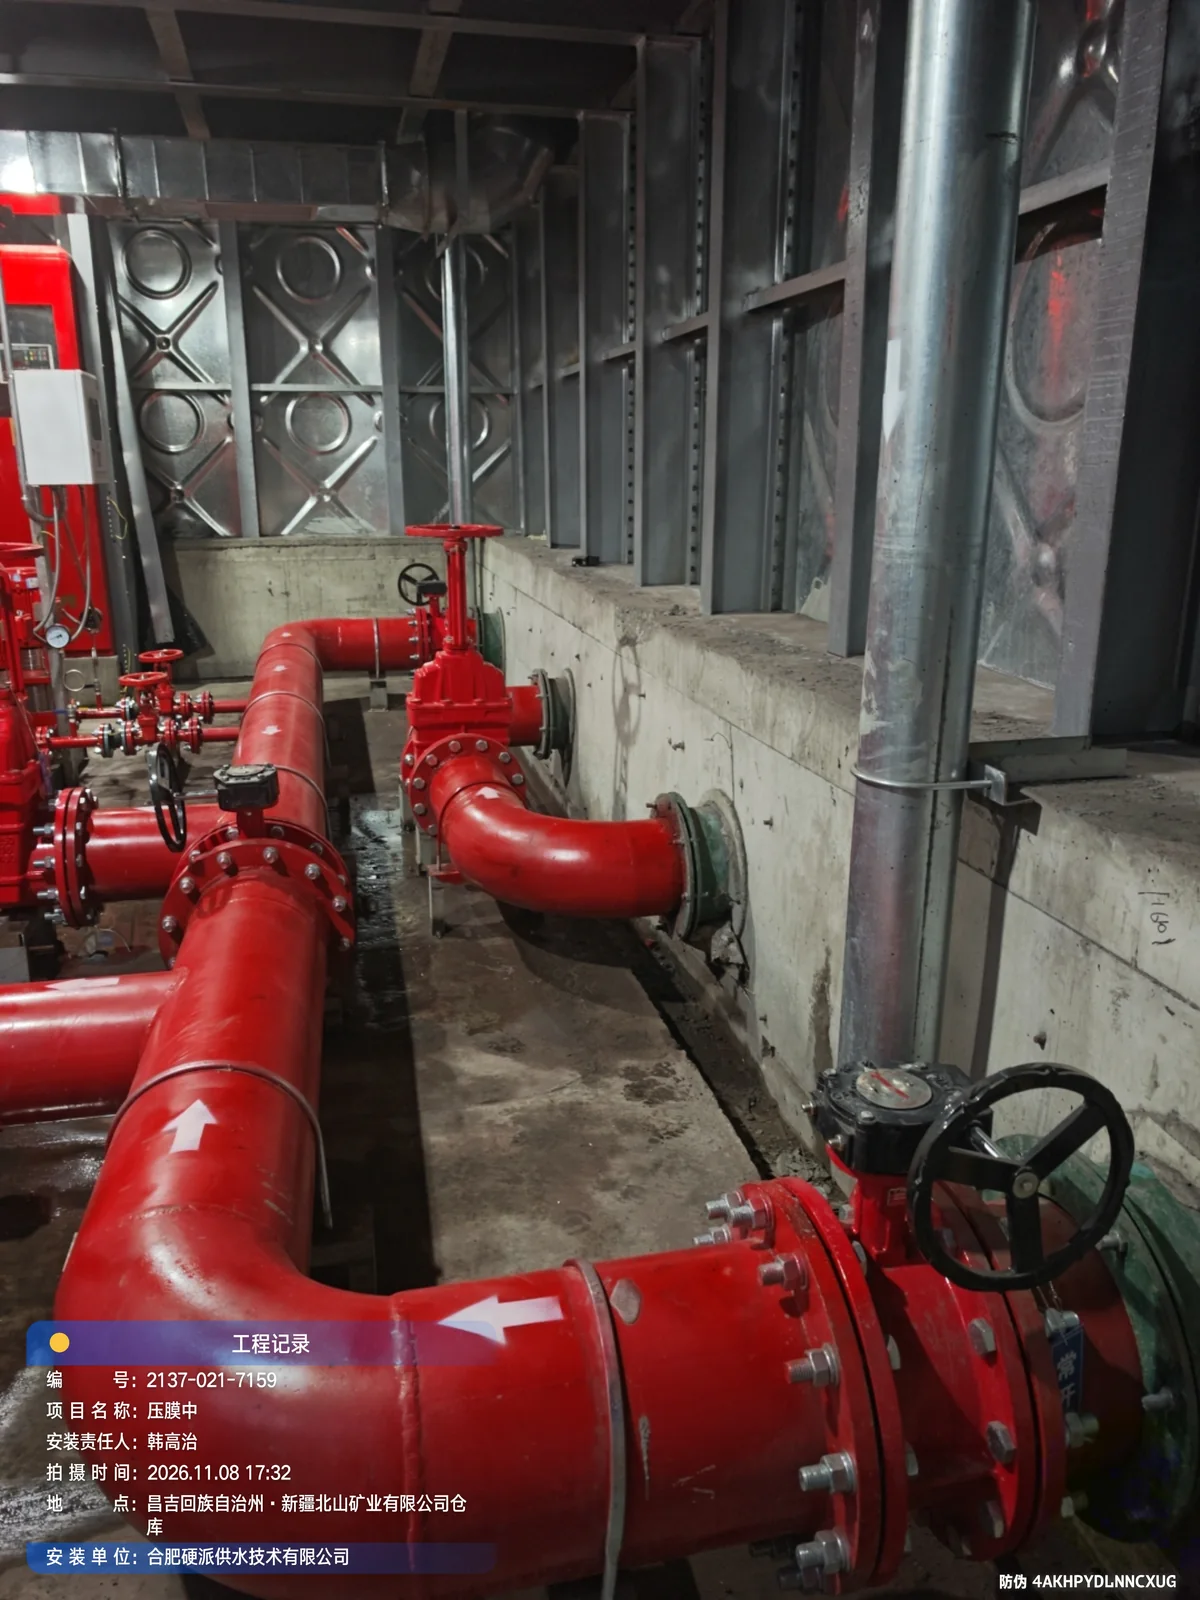
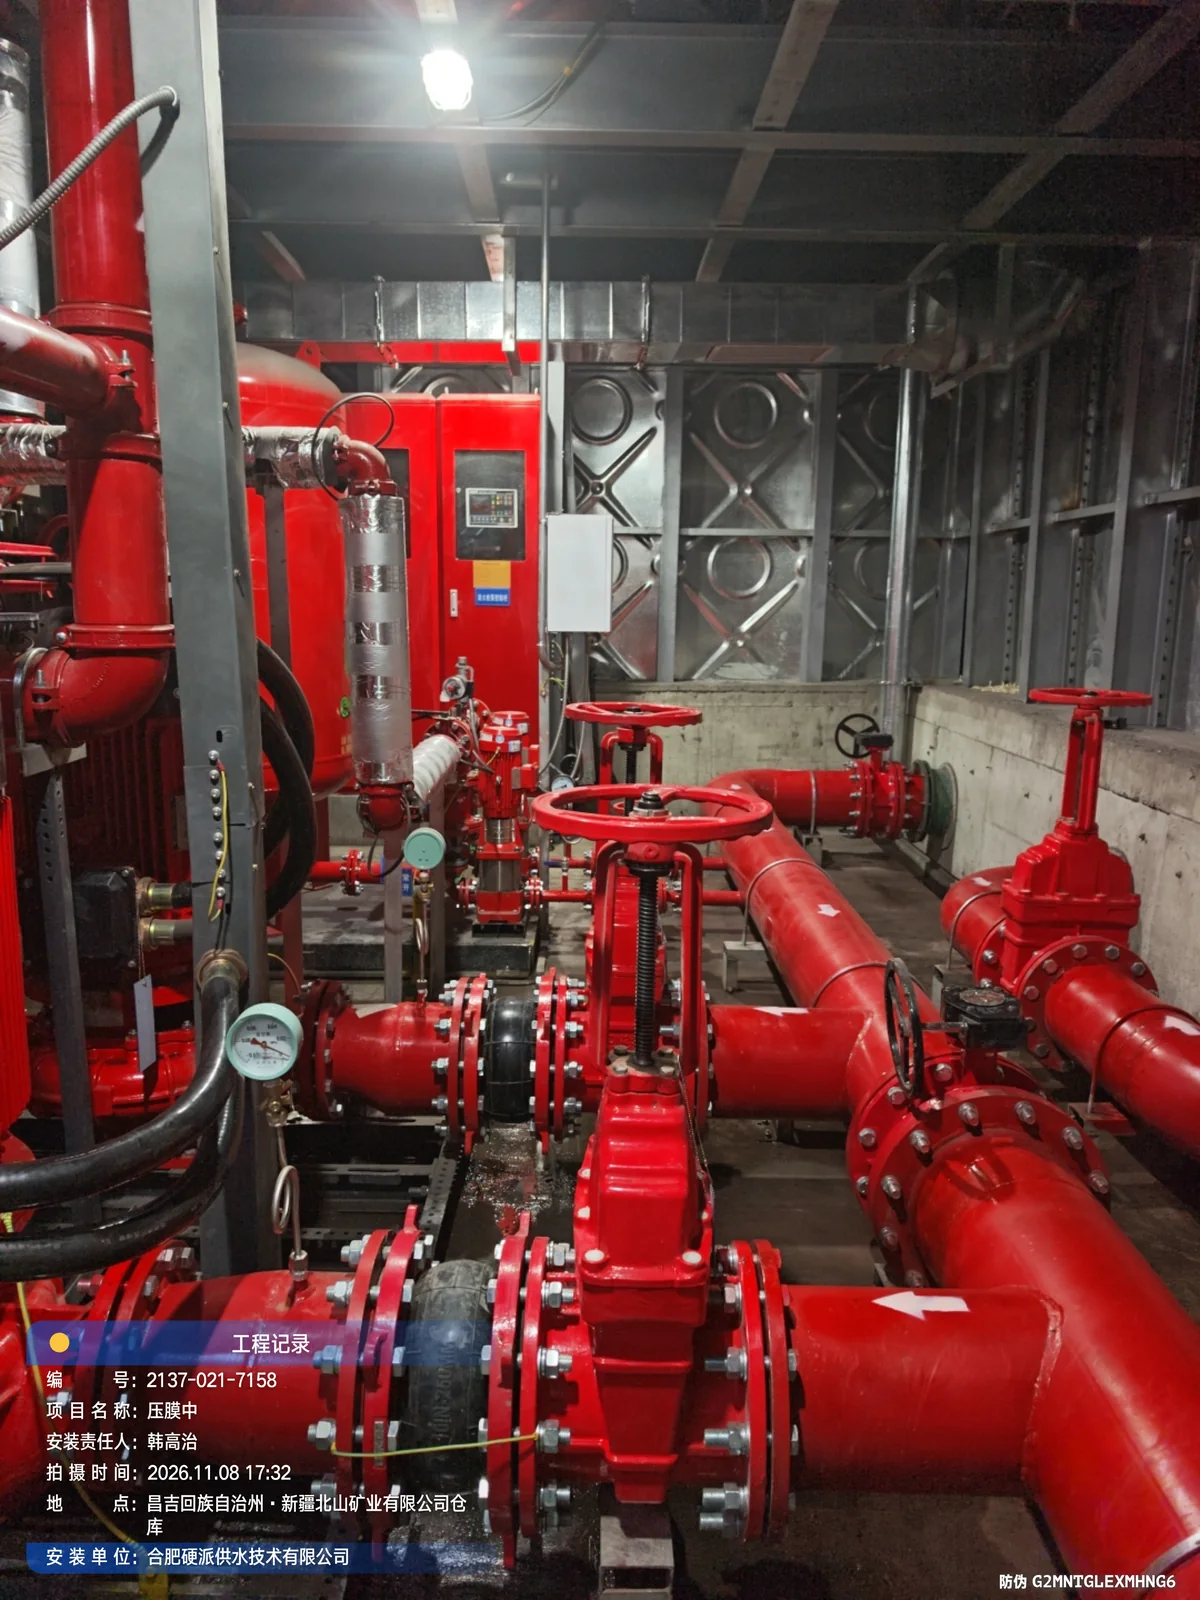
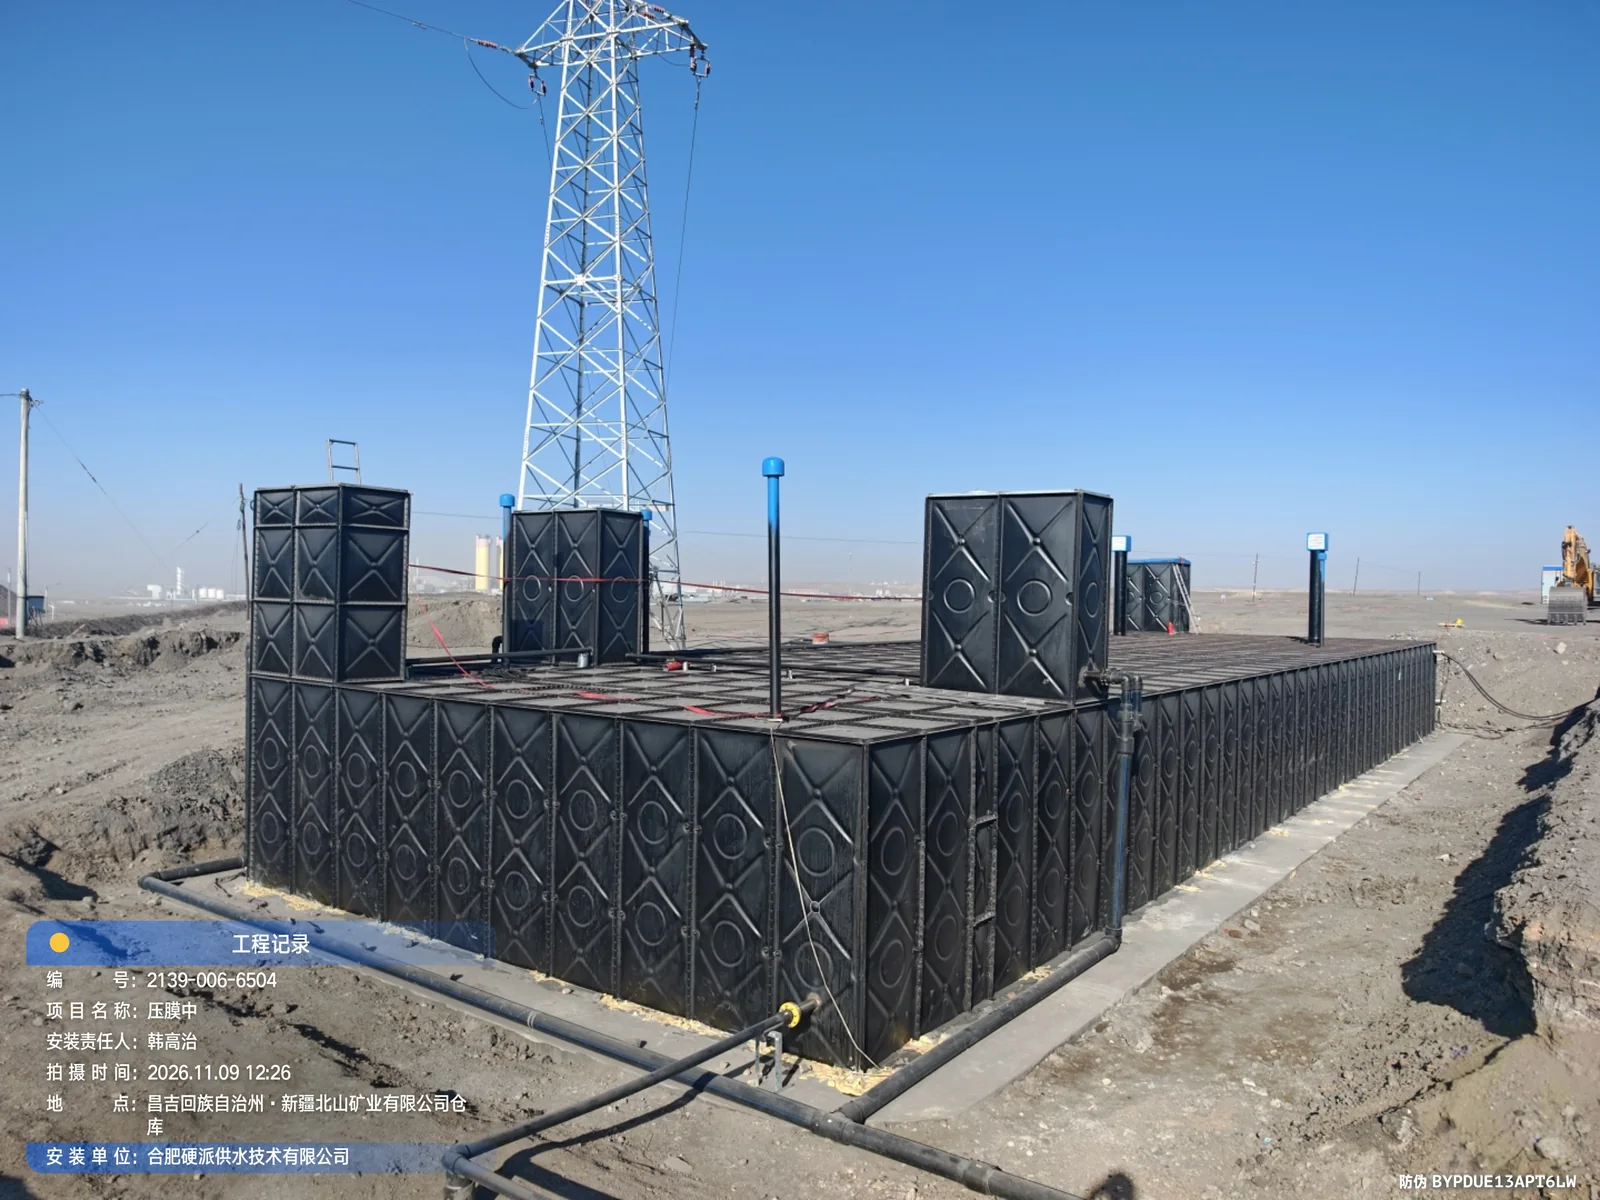
The project strictly follows the relevant standards for the selection and installation of 18CS01 prefabricated box pump integrated fire water supply pump station, MX smart pump station atlas, 19S204-1 atlas, and GB27898.3-2011 "Fixed Fire Water Supply Equipment Part 3: Fire Booster and Stabilized Pressure Water Supply Equipment". Among them, core electronically controlled pump equipment such as pump units, control cabinets, and inspection cabinets are independently produced by Dongfang Pump Industry; the overall placement of water tanks and pumping stations, on-site assembly construction, pipeline installation, system joint debugging, data compilation, and on-site acceptance cooperation are all handled by the EPANEL Water Supply team. The project completes the entire construction process in accordance with the requirements of the technical agreement and attached drawings, and is synchronized with complete quotation details to achieve one-stop delivery of equipment integration, on-site installation, commissioning and acceptance.
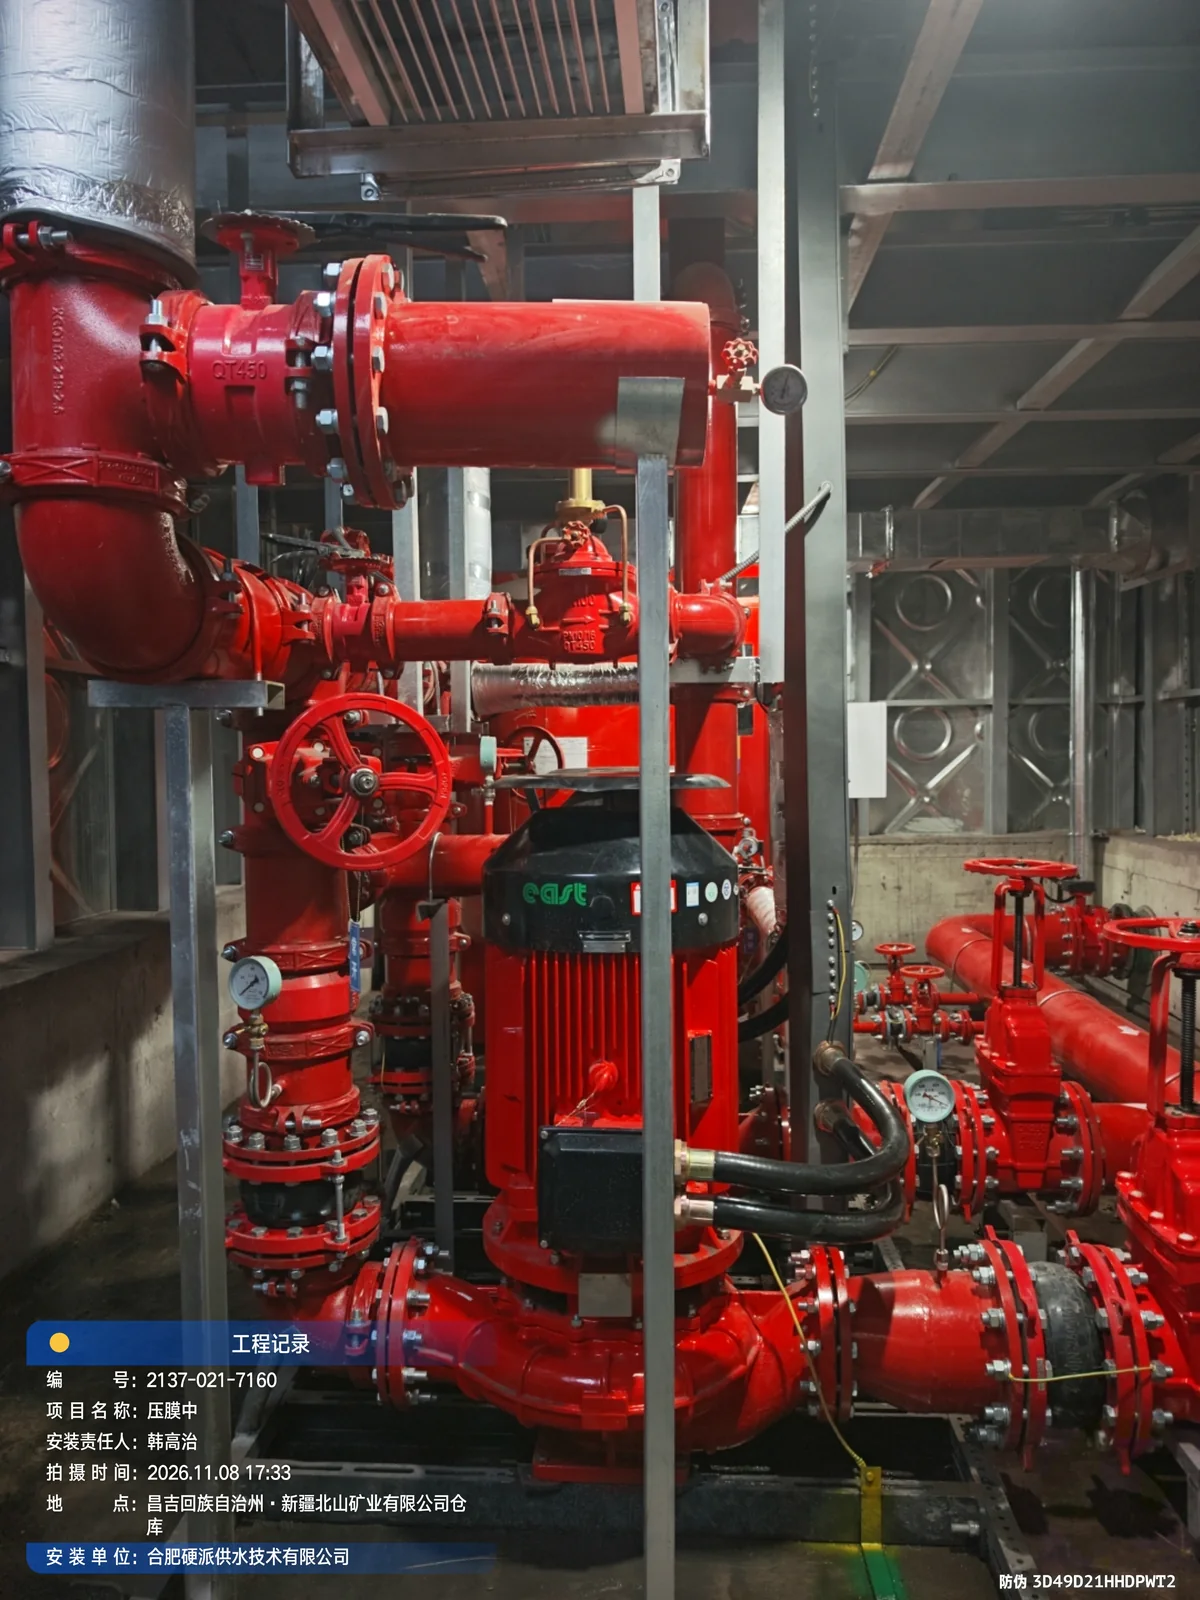
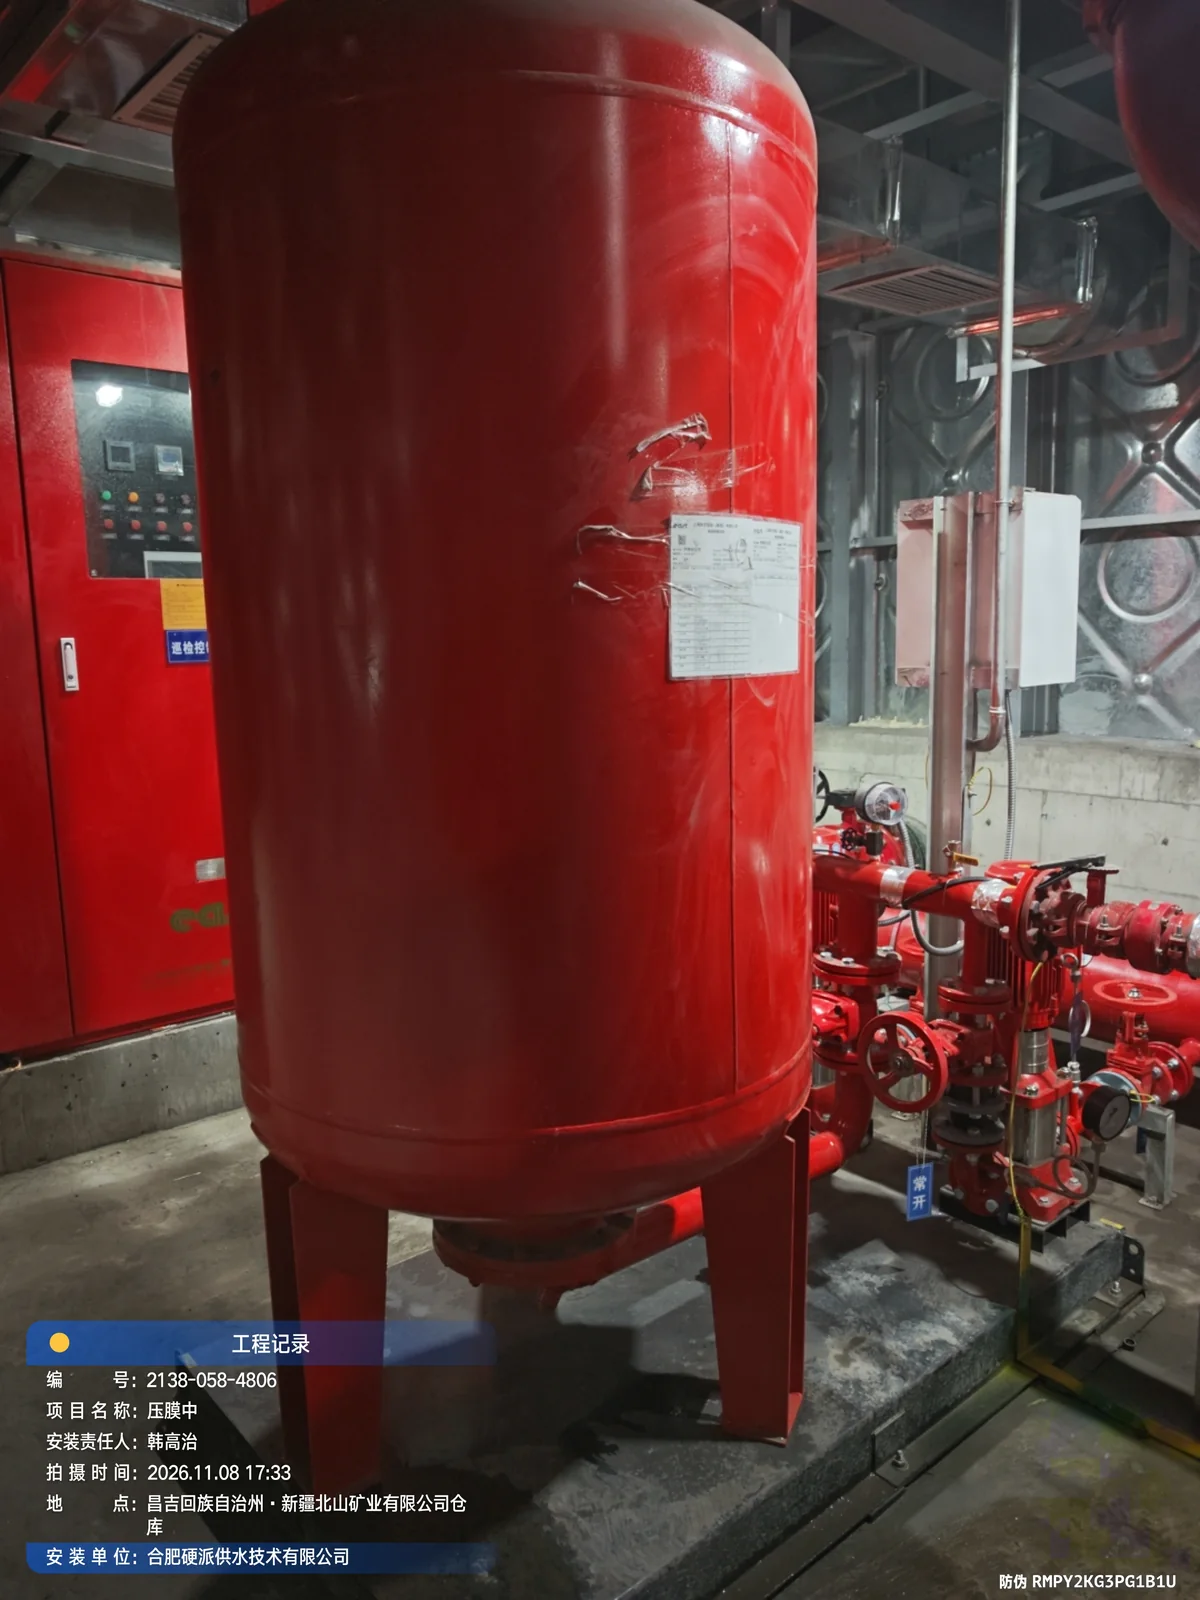
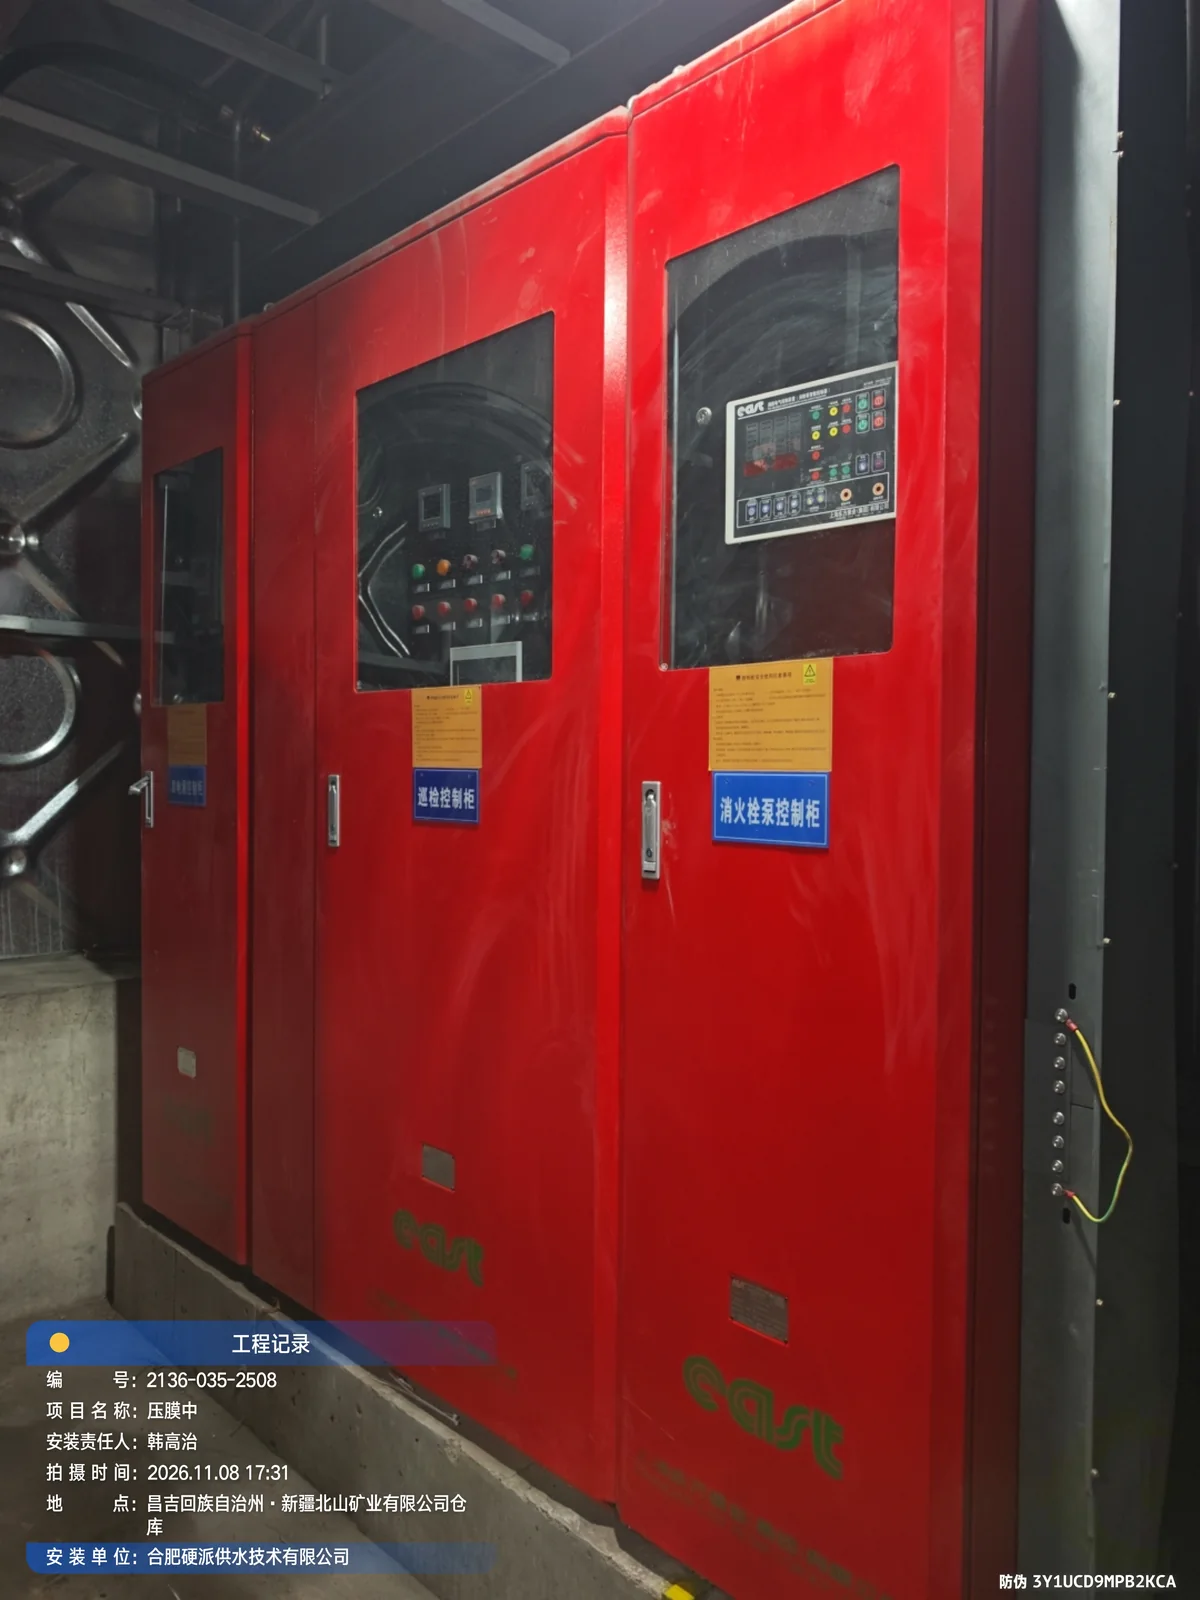
The fire water supply system in mining areas is a key infrastructure for safe production in mines. The implementation of this project fully leverages the advantages of the BDF prefabricated underground pumping station in its compact footprint, high integration, and convenient operation and maintenance. It adapts to the working conditions of the mining area and stably guarantees functions such as fire water supply, stable pressure water supply, and pump room drainage. EPANEL Water Supply will continue to develop complete sets of fire water supply solutions in the industrial and mining energy fields, and empower industrial and mining enterprises in the northwest region with standardized products and refined on-site construction for fire safety construction.