


 Back

Recently, the large-scale water storage tank project in Taolou Town, Changfeng County, Hefei, constructed by our company Hefei EPANEL Water Supply Technology Co., Ltd., has been fully completed and officially put into operation. With its excellent industrial design, top-notch anti-corrosion and insulation technology and intelligent monitoring and management system, this project has become a new benchmark for regional agricultural irrigation and industrial water infrastructure, providing a solid water supply guarantee for local rural revitalization and economic development.

The core of this project is multiple one thousand-cubic-meter-level cylindrical water storage tanks. Different from ordinary storage tanks, this series of products strictly follows industrial design standards, has extremely high mechanical strength and structural stability, and can safely withstand huge hydrostatic pressure and external loads.
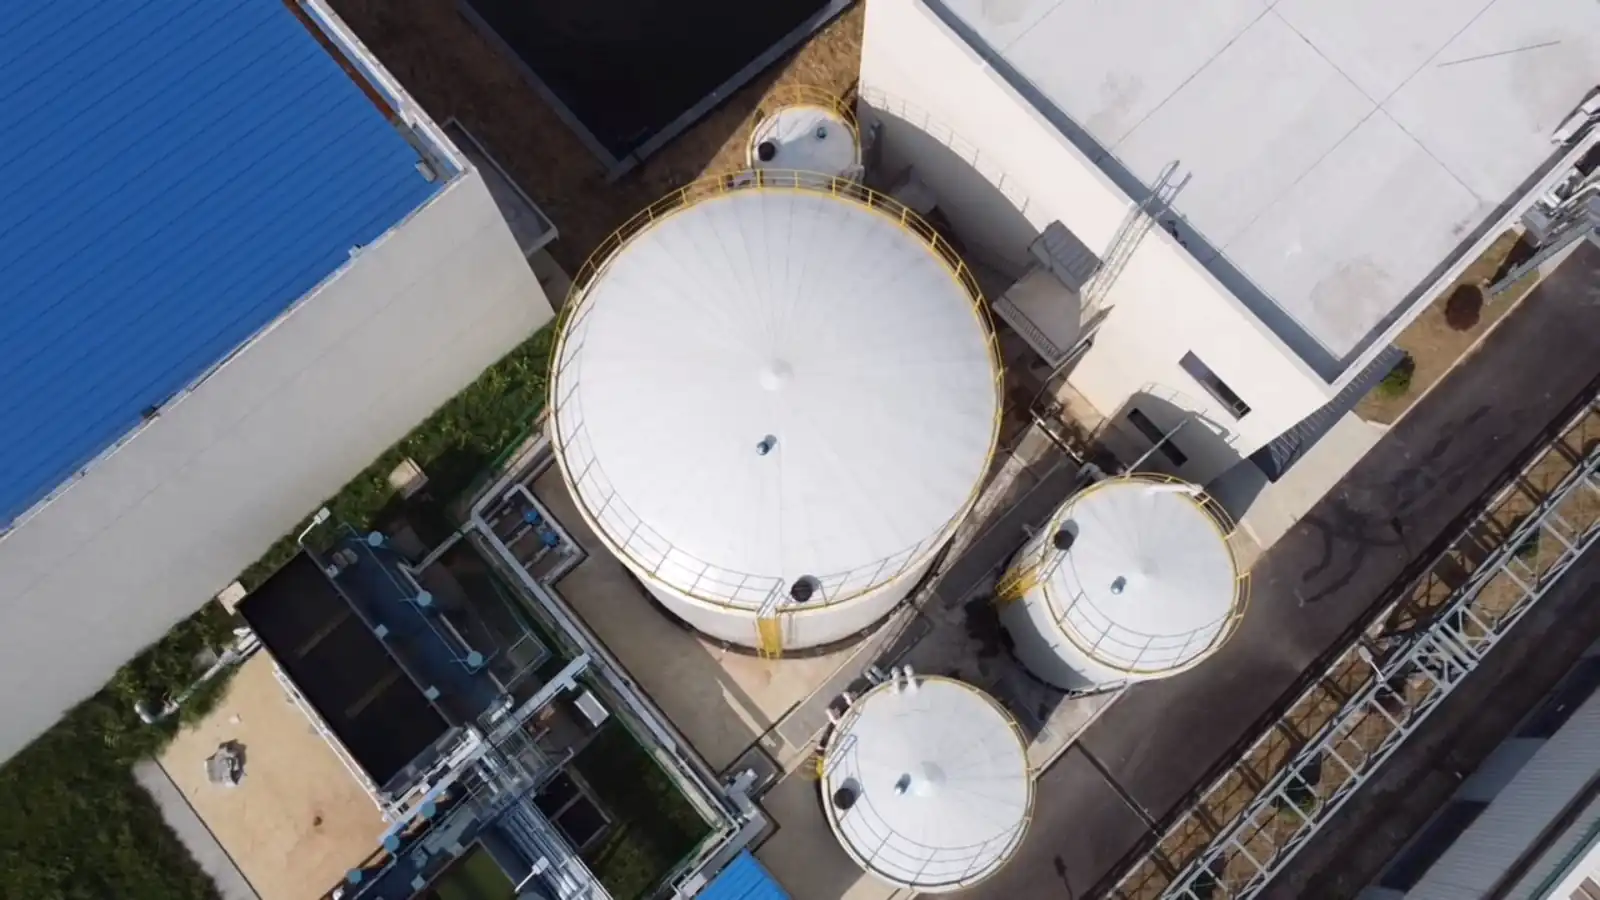
One of the highlights of the project process is its triple protection system:
Internal protection: The inner wall of the tank is coated with polyurea anti-corrosion coating. The material has excellent adhesion, wear resistance, corrosion resistance and non-toxic and harmless properties, fully ensuring the safety and cleanliness of stored water bodies.
External protection: The outer wall of the tank is made of epoxy coal pitch anti-corrosion layer. Its excellent weather resistance and chemical stability can effectively resist long-term erosion in complex outdoor environments.
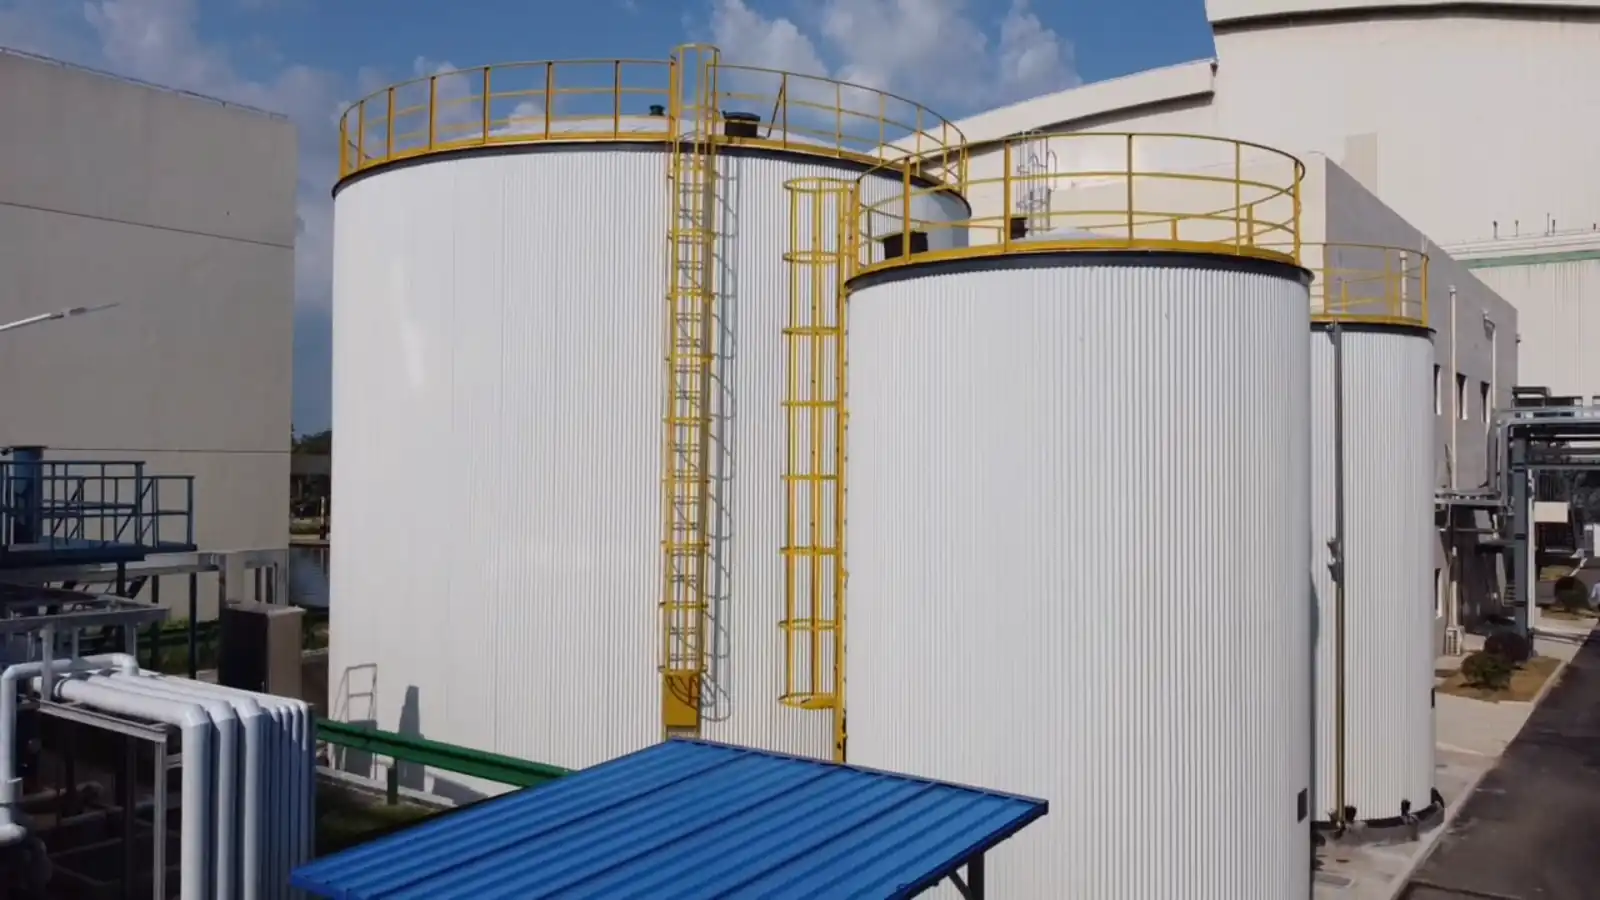
Insulation and energy saving: In addition to the anti-corrosion layer, an additional aluminum silicate insulation board is installed, which greatly reduces heat loss caused by ambient temperature differences and achieves high efficiency and energy saving in the water storage system.
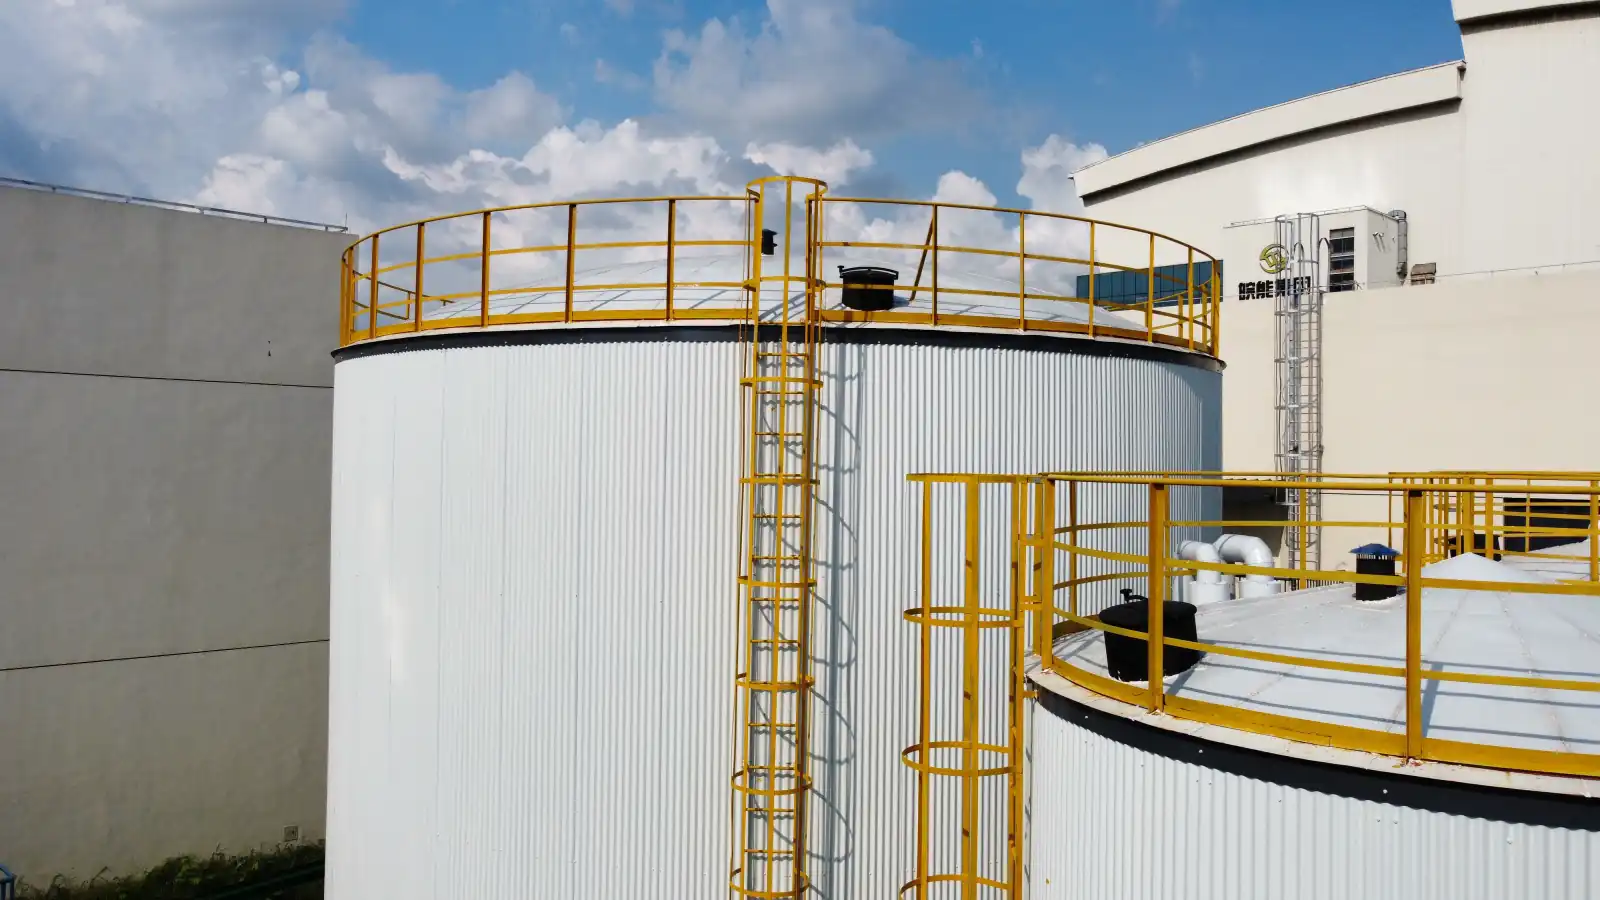
This water storage system is well designed and fully functional. Each water tank comes standard with top manholes, side manholes, water inlets, water outlets, overflow pipes, sewage outlets, exhaust pipes, top safety guardrails and hand-operated ladders, taking into account both operational convenience and maintenance safety.
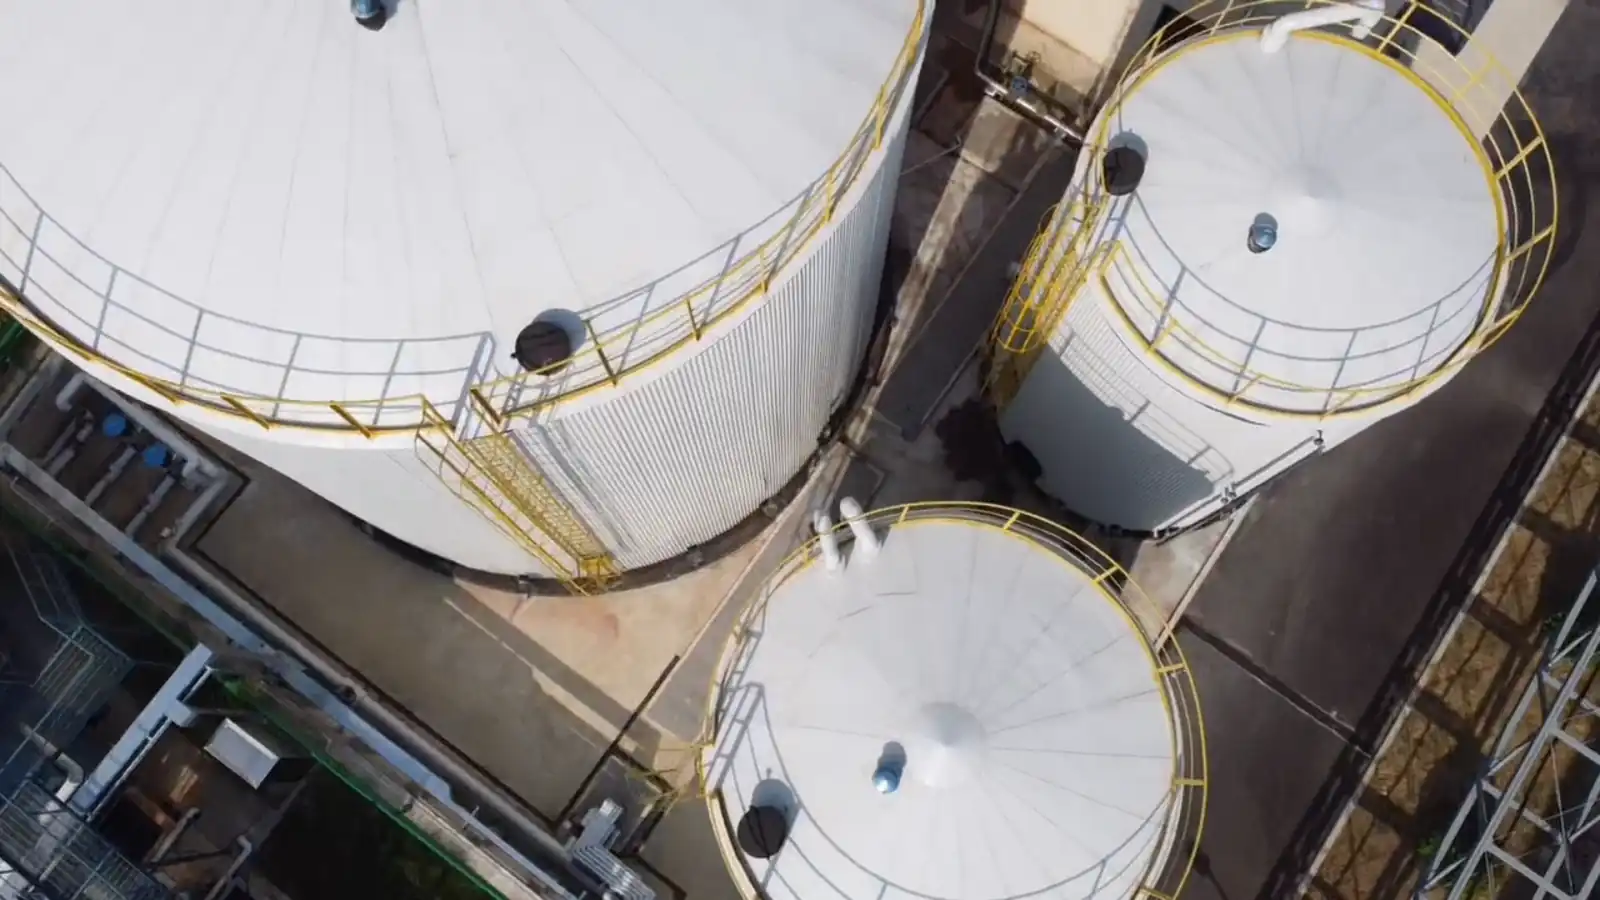
In terms of intelligence, the system comes standard with “on-site+"Far EasTone" dual liquid level monitoring system. Staff can either directly read the data on-site through the local display level gauge, or use the remote transmission system to conduct real-time water level monitoring and early warning in the remote central control room or mobile terminal, realizing unmanned duty and intelligent management.
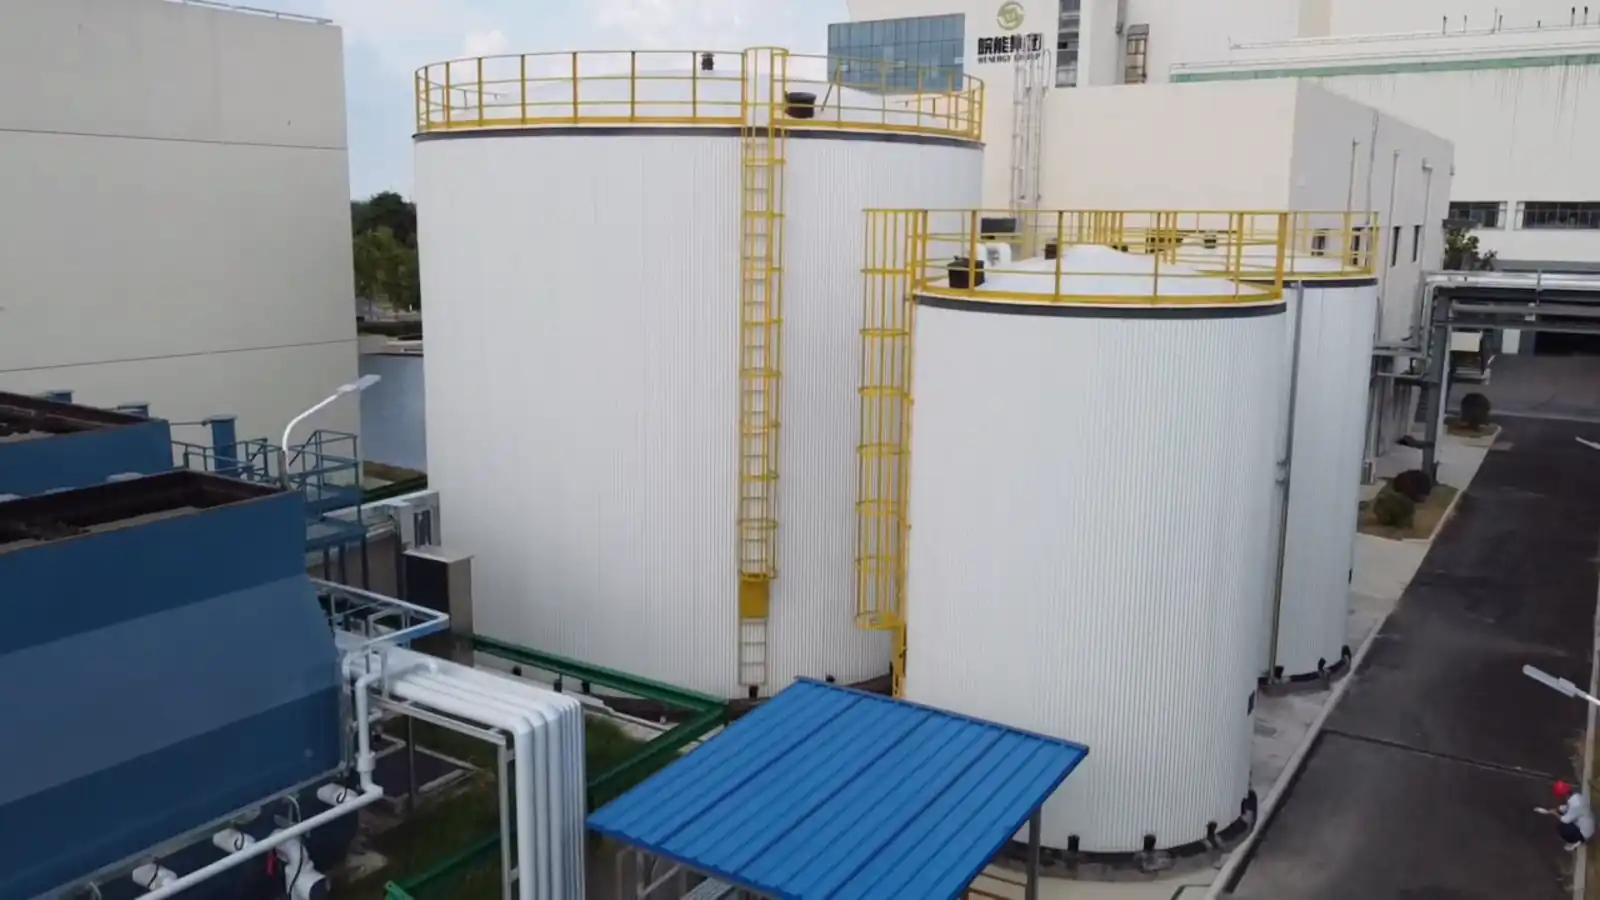
In addition, all interfaces and connecting piping systems of the water tank body adopt standardized flange connections. This design not only has excellent sealing performance, but also can effectively withstand and offset the stress and moment generated by the pipeline, fundamentally eliminating the risk of leakage caused by weak connection points, and ensuring the ultra-high reliability and stability of the long-term operation of the entire water supply system.
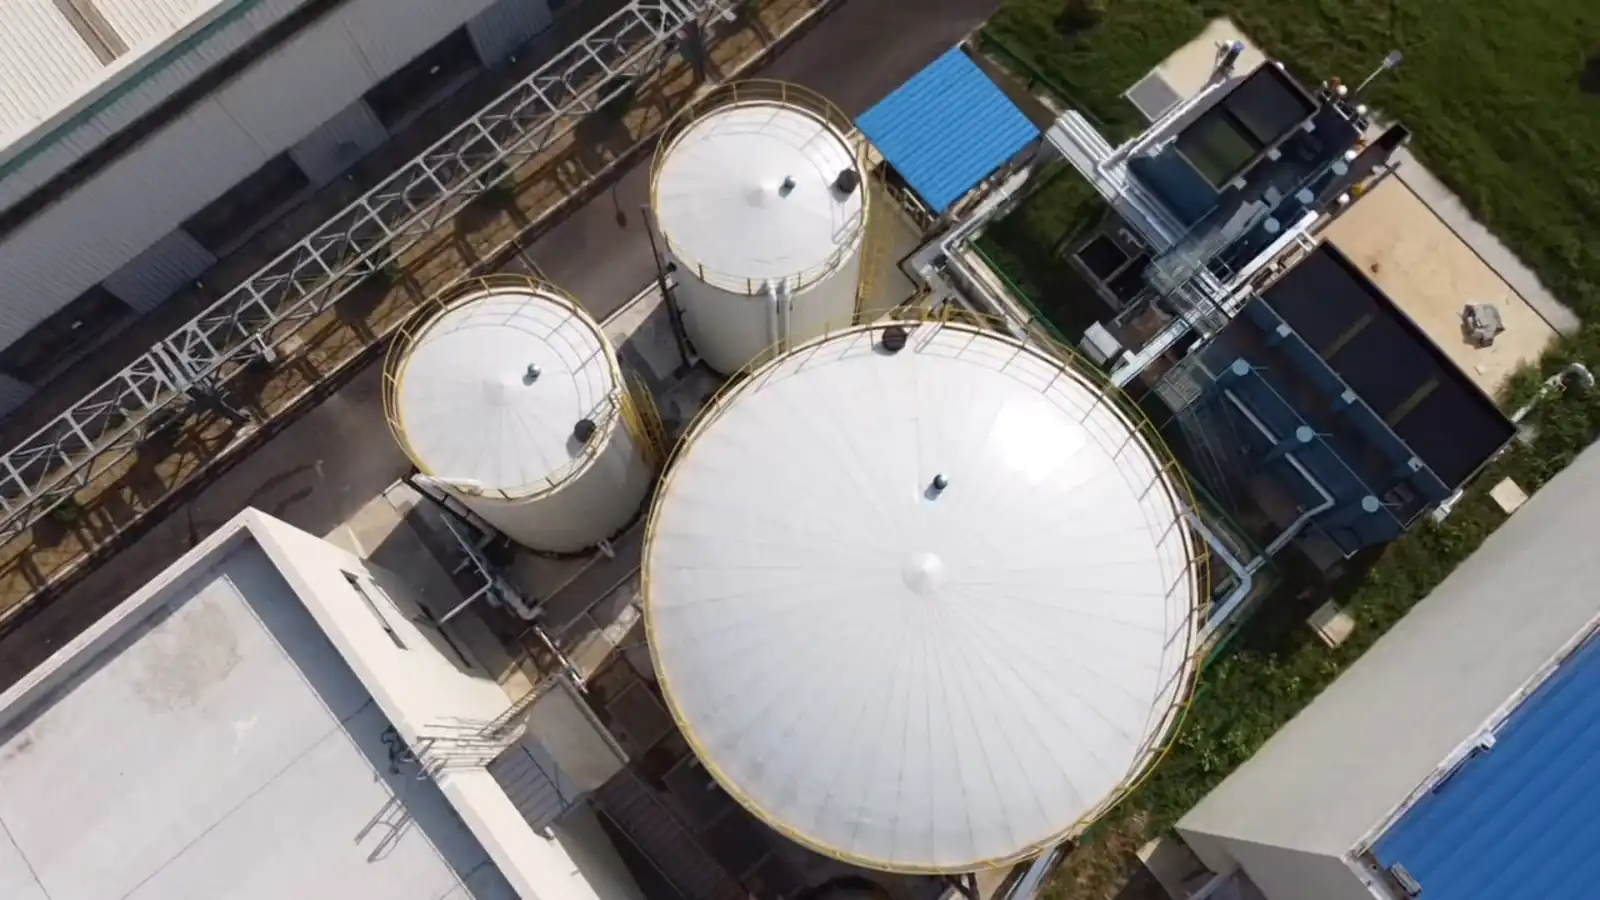
The successful implementation of this project fully proves Hefei EPANEL Water Supply Technology Co., Ltd.’s strong ability to provide one-stop solutions in the field of large-scale industrial water storage. With its excellent quality, this series of water storage tanks can be widely used in various scenarios such as agricultural irrigation, corporate production water, firefighting water reserve, and community water supply.

"We are committed to combining the most reliable industrial technology with the actual needs of customers." said the person in charge of the EPANEL project. "The success of the Taolou Town project is a microcosm of our deep penetration into the high-end water storage market. In the future, we will continue to rely on mature technology and rich project experience to provide professional and reliable water storage solutions to customers in more regions across the country."